- (801) 210-1303
- [email protected]
- Weekdays 9am - 5pm MST
The first step to securing funding is building a plan for your program. Let us help you get started.
A real CNC lathe plus a fault-setting electrical cabinet — programming, electrical design, debugging, and lathe maintenance training on one lab platform.
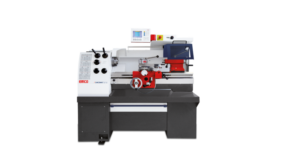
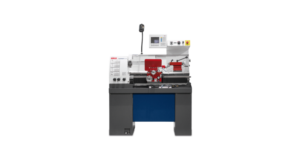
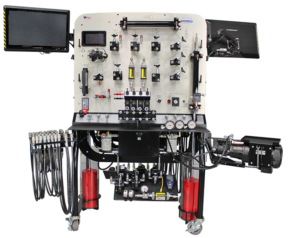
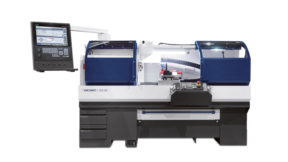
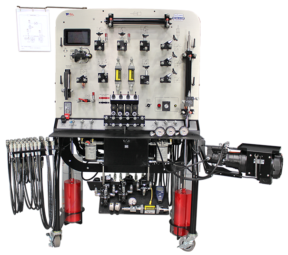
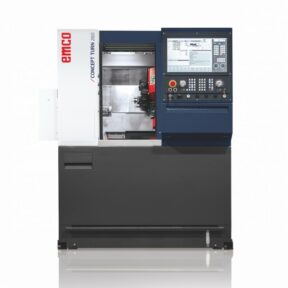
The CNC Turning Maintenance Experimental Platform combines a fault-setting electrical cabinet with a fully operational CNC lathe. Students program and machine parts on live hardware while also practicing CNC lathe maintenance and repair. It is intended for undergraduate and vocational colleges teaching CNC technology.
The modular cell covers CNC programming, electrical design, installation, debugging, and machine operation in one high-tech training system.
This is a standard CNC machine tool, not a desktop mock-up. Students can disassemble, adjust, and operate authentic hardware: two-phase hybrid stepping motor, high-speed constant-torque spindle, ball screw, origin/limit switch, electronic handwheel, and cooling water pump.
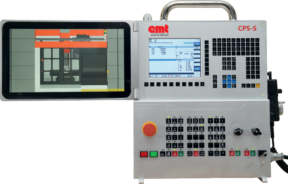
Key building blocks include the CNC system, spindle speed-control units, XZ motion-axis units, and switch input/output units. The lathe supports two-axis work from cylindrical and curved-neck turning through ball-head and thread cutting. Catalogue materials include steel, iron, copper, aluminum, plexiglass, plastic, and wax molds. The machine is described as compact, high-speed, and straightforward to operate.
| Item | Specification |
|---|---|
| Platform construction | Metal-plate integrated cabinet; electrical installation platform and controller plane in an L-shaped layout |
| Electrical installation platform | 220 × 100 cm |
| Mobility | 4 swivel casters with brakes |
| Electrical cabinet test bench (L × W × H) | 80 × 90 × 190 cm |
| Axes | 2-axis CNC turning with ball screws |
| Cooling | Yes — G-code controlled water pump |
| Handwheel | Hanging electronic handwheel (MPG) |
| Ball screw | Precision double-nut ball screw, heat treated and precision ground |
| CNC system | Siemens 808D Advance |
| Positioning accuracy | 0.03 mm |
| Repeatability | 0.02 mm |
| Maximum turning diameter | 210 mm |
| Maximum clamping diameter | 80 mm |
| X / Z travel | 80 mm / 290 mm |
| Spindle speed | Stepless 300–1,750 rpm ±10% |
| Maximum moving speed | 4,000 mm/min |
| Maximum feed speed, Z | 2,000 mm/min |
| Maximum feed speed, X | 2,000 mm/min |
| Electric turret | 4-position |
| Spindle through-hole | 20 mm |
| Thread turning | Yes |
| Spindle taper | Morse No. 4 (catalogue: “Mohs No. 4”) |
| Tailstock taper | Morse No. 2 (catalogue: “Mohs No. 2”) |
| Motor-driver resolution | 0.0025 m (as printed; confirm unit with EMT — likely 0.0025 mm) |
| Spindle output power | 1,100 W |
| Power requirement | 3-phase 380 V |